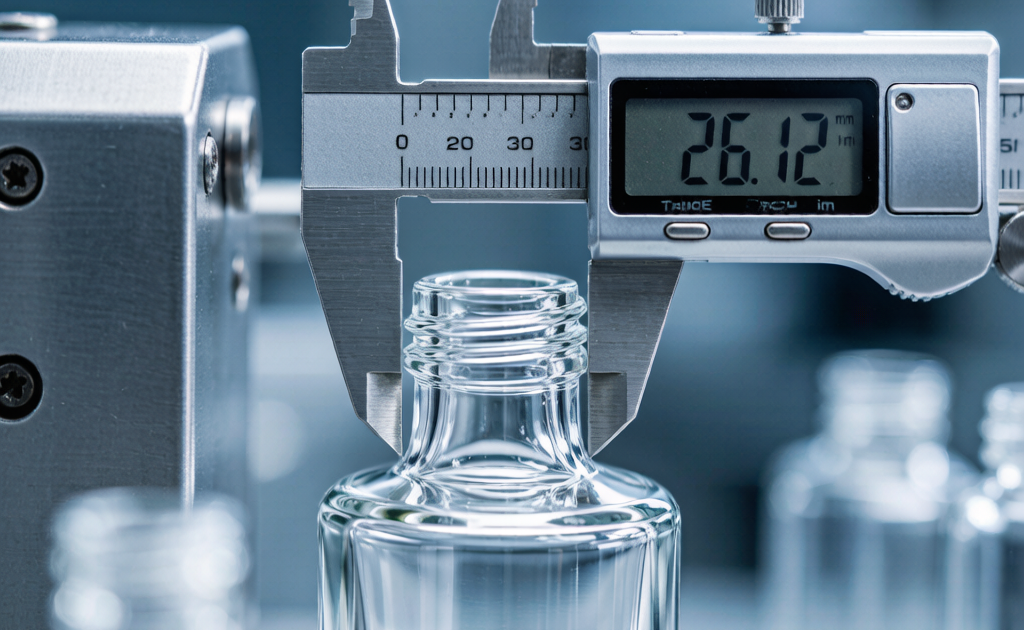
A perfume bottle neck that is 0.2mm too wide means your spray pump falls off during shipping. A base that is 0.15mm uneven means bottles wobble on the filling line. At our Huanshi factory, we have measured these failures firsthand. In glass bottle manufacturing, the difference between a premium product and a defective one often comes down to tolerances smaller than a human hair.
If you are sourcing custom perfume glass bottles, understanding dimensional tolerances is not optional. It is the single most technical specification that separates a smooth production run from a disaster. This guide breaks down what tolerances matter, why they matter, and how to specify them when ordering from any glass bottle factory.
What Is Glass Bottle Tolerance and Why Does It Exist?
Glass is not metal. You cannot machine it to ±0.01mm. Glass bottles are formed by blowing molten glass into a mold — a process called Individual Section (IS) machine blowing. The glass starts at 1,100°C and cools to room temperature. During that cooling, glass shrinks by roughly 10%. That shrinkage is not perfectly uniform. Variables like glass temperature, mold temperature, blow pressure, and cooling rate all introduce variation.
According to ASTM International standards C1036 (the standard for flat glass tolerances) and industry practices for container glass, manufacturers define acceptable dimensional ranges for each bottle parameter. These ranges are called tolerances. A ±0.3mm tolerance on the neck diameter means the factory guarantees every bottle will measure within 0.3mm above or below the target dimension.
The tighter the tolerance, the harder the production. A ±0.1mm tolerance on neck diameter might require:
- Mold cavity precision within ±0.05mm
- Glass temperature variance under ±5°C
- Blow pressure controlled to ±0.2 bar
- Cooling airflow calibrated per station
That level of control costs money. A factory offering ±0.1mm tolerance will charge 20-40% more than one offering ±0.5mm.
Key Dimensions and Industry-Standard Tolerances
Here are the critical dimensions on a perfume bottle and their typical tolerance ranges:
| Dimension | Standard Tolerance | Precision Tolerance | Impact of Failure |
|---|---|---|---|
| Neck inner diameter (ID) | ±0.3mm | ±0.1mm | Pump fit — loose or stuck |
| Neck outer diameter (OD) | ±0.3mm | ±0.1mm | Cap fit — wobble or crack |
| Neck height | ±0.5mm | ±0.2mm | Crimping height — leaks |
| Overall height | ±1.0mm | ±0.5mm | Filling line jamming |
| Body diameter | ±0.5mm | ±0.3mm | Label alignment off |
| Base flatness | ±0.4mm | ±0.15mm | Bottle wobbles on shelf |
| Wall thickness | ±0.3mm | ±0.15mm | Breakage, thermal shock |
| Total weight | ±3g (50ml) | ±1.5g (50ml) | Cost, perceived quality |
The Neck: Where Tolerance Makes or Breaks the Product
The neck is the most critical dimension on a perfume bottle. It interfaces with the spray pump and the cap. If the neck inner diameter is 0.2mm too large, the pump collar will not grip properly. The pump will push down during shipping, dumping fragrance into the carton. If the neck OD is 0.15mm too small, the cap will not seat fully, and the bottle will look crooked on the retail shelf.
FEA (Finite Element Analysis) and Crimping Geometry
When a pump is crimped onto a bottle neck, the brass collar deforms inward. The deformation must match the neck’s geometry. European Pharmacopoeia glass standards standards for container necks reference specific crimping profiles. The most common in perfume packaging is the 15mm DIN 18-style crimp neck — a standardized neck finish used across the industry.
For this neck type, the critical measurements are:
- Neck ID: Must allow the pump dip tube to pass through without friction. Target: 7.8mm ± 0.1mm.
- Neck OD: Must match the crimp collar diameter. Target: 15.0mm ± 0.15mm.
- Neck ring height: The locking ring that holds the crimp. Target: 2.5mm ± 0.2mm.
- Neck taper angle: The slight angle that guides the pump insertion. Target: 3° ± 1°.
When any of these drifts out of tolerance, you get field failures. We once tracked a batch of 8,000 bottles where the neck ID ran 0.25mm oversize. The result: a 4% pump ejection rate during transport. The client lost $12,000 in product damage and had to air-freight a replacement batch.
Wall Thickness: The Hidden Variable
Wall thickness tolerance affects three things: breakage rate, perceived quality, and thermal shock resistance.
Thin walls (under 1.5mm on a 50ml bottle) save glass. They make the bottle lighter. But they also make it fragile. A bottle with 1.2mm walls will shatter if dropped from 60cm onto tile. A bottle with 3.0mm walls (heavy base style) will survive a 1.5-meter drop.
More importantly, inconsistent wall thickness causes thermal shock failure. If one side of the bottle is 2.0mm thick and the other is 1.2mm, the thick side holds heat longer during annealing. When the bottle cools, thermal stress builds at the thickness transition. Drop the bottle in cold water — or fill it with cold fragrance — and it cracks along the stress line.
How We Control Wall Thickness at Huanshi
Our process uses three checkpoints:
- Mold design: We use CAD simulation to predict glass distribution before cutting the mold. The software (Nürnberg-style glass flow simulation) predicts wall thickness to within 0.1mm.
- Blow pressure calibration: Each IS machine station is calibrated daily. We measure blow pressure with a digital transducer accurate to ±0.05 bar.
- Post-production gauging: Every 200th bottle goes through a wall thickness gauge (sonic resonance type). We log the data and run SPC (statistical process control) charts to catch drift before it becomes a problem.
How Tolerance Affects Your Filling Line
If you are a brand owner sending bottles to a contract filler, tolerance directly impacts your filling efficiency. Here is what happens when bottles arrive out of spec:
| Problem | Tolerance Issue | Filling Line Impact |
|---|---|---|
| Bottles too tall | Overall height +1.5mm over spec | Capping station jams, 3-5% downtime |
| Neck ID too small | Neck ID -0.3mm under spec | Pump insertion fails, manual rework |
| Base uneven | Base flatness >0.4mm | Conveyor guide rails misalign, tip-overs |
| Weight too heavy | Weight +5g over spec | Filler level sensor miscalibrates |
| Neck OD too large | Neck OD +0.4mm over spec | Cap cracks during press-fit |
A contract filler running 60 bottles per minute loses roughly $45 per minute of downtime. A 5% reject rate on a 20,000-bottle run costs $900 in wasted filling time alone — before counting the cost of the bottles, fragrance, and packaging.
Specifying Tolerances in Your Purchase Order
Most buyers specify only the bottle dimensions (height, diameter, capacity). They leave tolerance to the factory. That is a mistake. Here is what a proper tolerance specification looks like:
“`
Bottle: 50ml Eau de Parfum
Overall height: 158mm ± 0.5mm
Body diameter: 54mm ± 0.3mm
Neck ID: 7.8mm ± 0.1mm
Neck OD: 15.0mm ± 0.15mm
Neck ring height: 2.5mm ± 0.2mm
Base flatness: < 0.2mm deviation
Wall thickness (body): 2.0mm ± 0.2mm
Wall thickness (base): 5.0mm ± 0.5mm
Total weight: 145g ± 2g
Inspection standard: ISO 9001 quality management 2859-1, General Inspection Level II
AQL: 2.5 major / 4.0 minor
“`
When you hand a spec sheet like this to a supplier, three things happen. First, they quote you accurately — they know what level of precision you expect. Second, they respect you — a buyer who specifies tolerances is a buyer who will check them. Third, you have a contractual basis for rejecting out-of-spec goods.
Tolerance vs Cost: Finding the Sweet Spot
Tighter tolerances cost more. But over-specifying tolerance wastes money. Here is a practical guide:
- ±0.1mm tolerance: Only needed for neck dimensions that interface with pumps/caps. Justifies 15-20% cost premium.
- ±0.3mm tolerance: Appropriate for body diameter and visible dimensions. Standard cost.
- ±0.5mm tolerance: Fine for overall height and non-critical dimensions. No cost premium.
- ±1.0mm tolerance: Acceptable for capacity-related dimensions (fill height) when the filler adjusts by volume, not height.
Do not demand ±0.1mm on the overall height. It adds cost without value. Do not accept ±1.0mm on the neck ID. It guarantees filling line problems.
Why Huanshi Invests in Precision
Our tolerance capabilities meet FEVE European Container Glass Federation (the European Container Glass Federation) quality benchmarks. We achieve ±0.1mm on neck dimensions on our IS machine line through:
- Daily mold cavity inspection with digital calipers (Mitutoyo, 0.01mm resolution)
- Glass temperature monitoring at the feeder (target: 1,150°C ± 5°C)
- Blow pressure SPC with Cpk targets above 1.33 on critical dimensions
- Annealing lehr profile verification (550°C peak, 2.5-hour cycle)
If you want to learn more about how our glass annealing process ensures tolerance stability, or how our 12-checkpoint QC system catches dimensional drift before shipment, those guides walk through our process in detail.
Frequently Asked Questions
What is the standard tolerance for perfume bottle neck diameter?
The industry standard tolerance for perfume bottle neck diameter is ±0.3mm. For precision applications where the neck interfaces directly with a crimp-on spray pump, a tighter tolerance of ±0.1mm is recommended. At Huanshi, we hold ±0.1mm on neck ID and ±0.15mm on neck OD for all custom perfume bottle orders.
Why does wall thickness tolerance matter for perfume bottles?
Wall thickness tolerance directly affects breakage rate, thermal shock resistance, and perceived quality. Uneven wall thickness (e.g., 2.0mm on one side, 1.2mm on the other) creates thermal stress during annealing. When the bottle is filled with cold fragrance or dropped, it cracks along the stress line. Standard wall thickness tolerance is ±0.3mm; precision tolerance is ±0.15mm.
How tight should tolerances be on a custom perfume bottle order?
Specify ±0.1mm only for neck dimensions that interface with pumps and caps. Use ±0.3mm for body diameter and visible dimensions. Accept ±0.5mm for overall height. Do not over-specify — demanding ±0.1mm on overall height adds 20%+ cost with no practical benefit. Match tolerance to functional need.
What inspection standard should I use for perfume bottle tolerance verification?
Use ISO 2859-1 (sampling procedures for inspection by attributes) at General Inspection Level II. Set AQL at 2.5 for major defects (dimensions that affect pump/cap fit, base flatness) and 4.0 for minor defects (cosmetic dimensions, weight). Request an OQC (Outgoing Quality Control) report with each shipment showing actual measurements against your spec sheet.
How much does tighter tolerance increase the cost of perfume bottles?
Tightening tolerance from standard (±0.3mm) to precision (±0.1mm) on neck dimensions typically increases unit cost by 15-25%. This covers mold precision upgrades, increased QC sampling, and higher reject rates. The cost increase is justified for neck and base dimensions where failures directly impact product performance, but unnecessary for non-critical dimensions.
—
Precision is not a luxury in perfume bottle manufacturing. It is the difference between a product that performs and one that fails. At Huanshi, we measure down to 0.01mm because we have seen what 0.1mm of drift can cost our clients. Send us your tolerance requirements — we will show you our capability report and sample data before you commit. Get a precision quote today.

